Case Study · CNC Turning
Turned Stainless Component
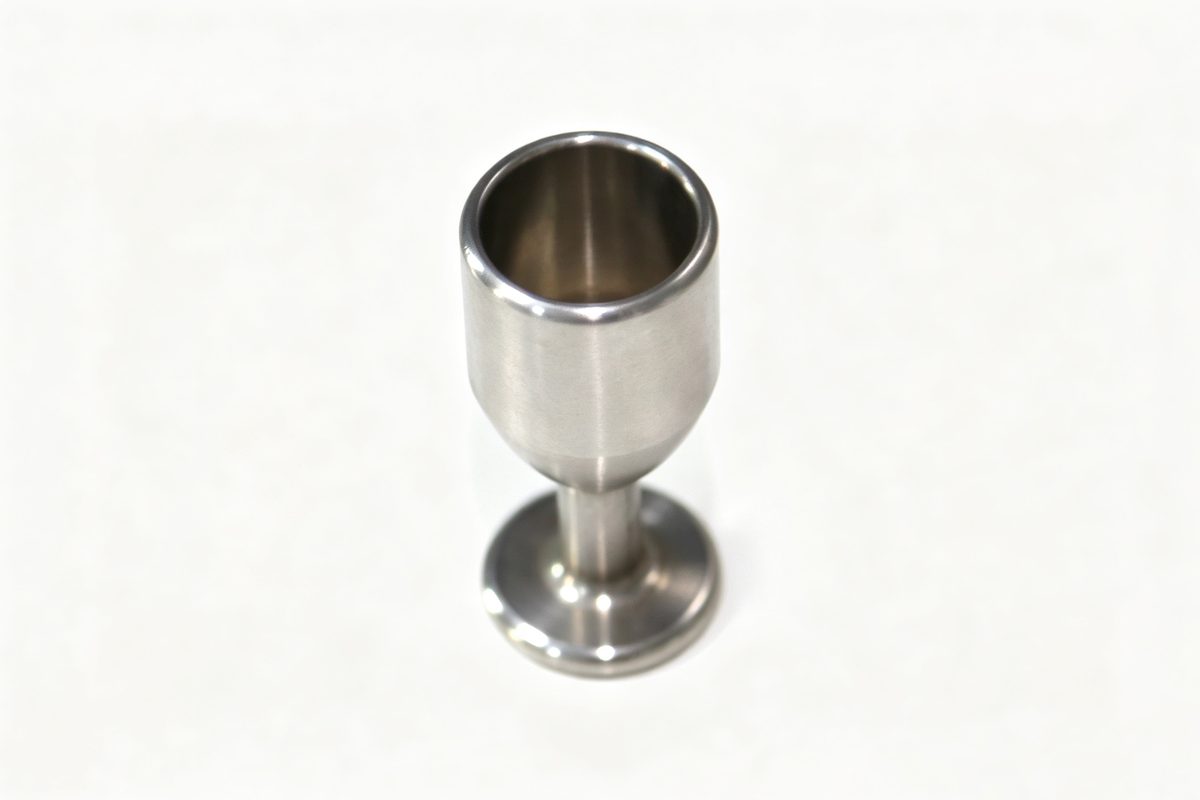
A 316 stainless cup with a 1.2 mm wall, where the wall thickness and the run-out at the open end decided which machine the part could be made on.
Problem
The bore drifted through the shift
Turning a 1.2 mm wall in 316L invites chatter and spring-back. The previous supplier held the bore but lost the run-out at the open end, so the part would not seat in the assembly.
Approach
Complete in one spindle, gauged in process
The part was moved to a lathe with a subspindle, so the second operation happened without re-chucking. Cutting parameters and support were set for the thin wall rather than for cycle time.
- Subspindle transfer, no re-chuck
- Run-out checked at the open end
- Wall thickness verified by ultrasonic gauge
- Passivation after machining
Result
Capability held through the shift
Run-out stayed inside 0.015 mm across the batch, and the parts seated without selection. The part has been reordered four times on the same route.
Drawings and customer name stay confidential.
More projects
Related case studies
Molded Plastic Enclosure
Two-part ABS enclosure with a gasket groove molded in, matched to a silicone seal.
View Case Study
Automation Fixture Bracket
Bracket machined from solid, flatness and hole position held for a locating fixture.
View Case Study
Extruded Silicone Tubing
Small-diameter tubing extruded to a consistent wall, then cut and packed to length.
View Case StudyReady to Start Your Precision Component Project?
Send us your drawing and requirements for an engineering review and quotation.