Case Study · CNC Machining
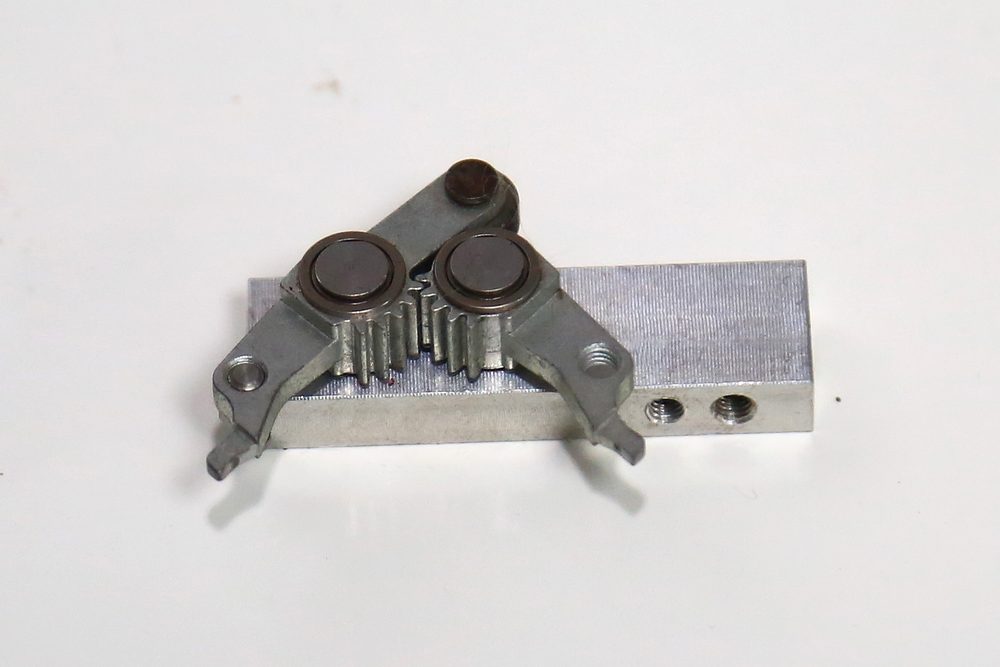
Automation Fixture Bracket
A locating bracket for an automation fixture, where flatness across the mounting face mattered more than any single dimension.
Problem
The weld moved the datum
The bracket was flat when machined and not flat after anodizing. The fixture would not seat without shimming, which the customer would not accept on a production line.
Approach
One part, machined from solid
Material was stress-relieved before finishing, and the mounting face was machined after anodizing to remove the coating build-up on the critical surface.
- Stress relief before finishing
- Mounting face machined after coating
- Flatness check on a surface plate
- Hole position verified on CMM
Result
Shimming stopped
The bracket seats without shimming, and the customer has standardised the fixture design around it.
Drawings and customer name stay confidential.
More projects
Related case studies
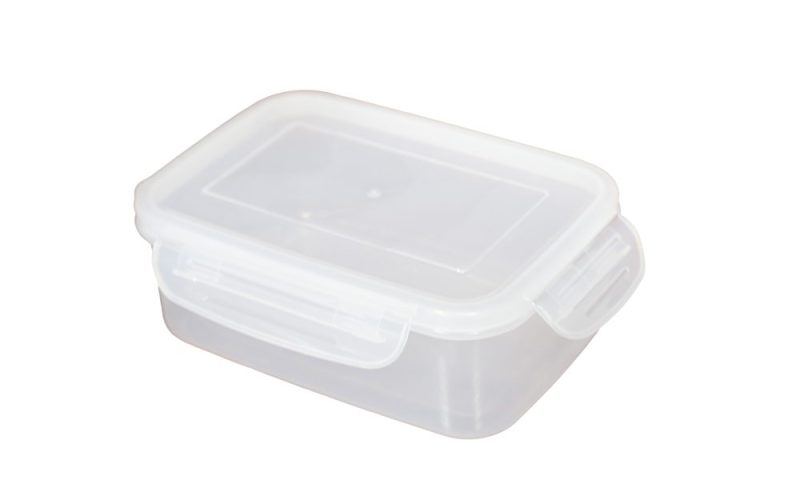
Molded Plastic Enclosure
Two-part ABS enclosure with a gasket groove molded in, matched to a silicone seal.
View Case Study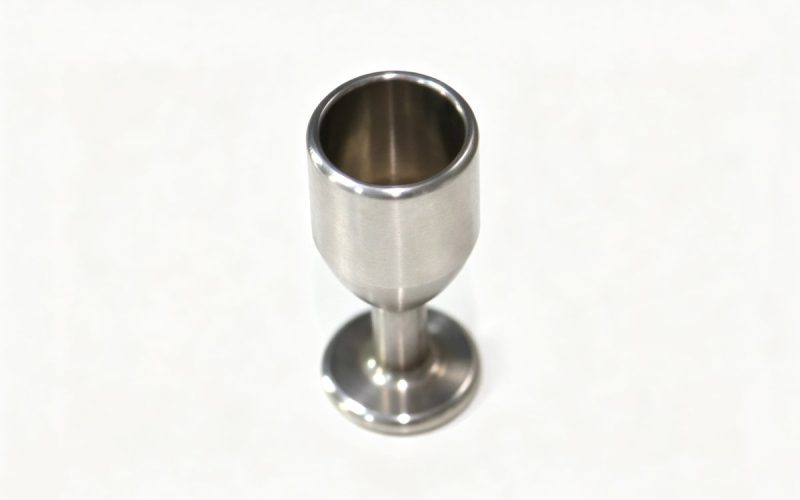
Turned Stainless Component
Thin-wall turned part where wall thickness and run-out decided the process route.
View Case Study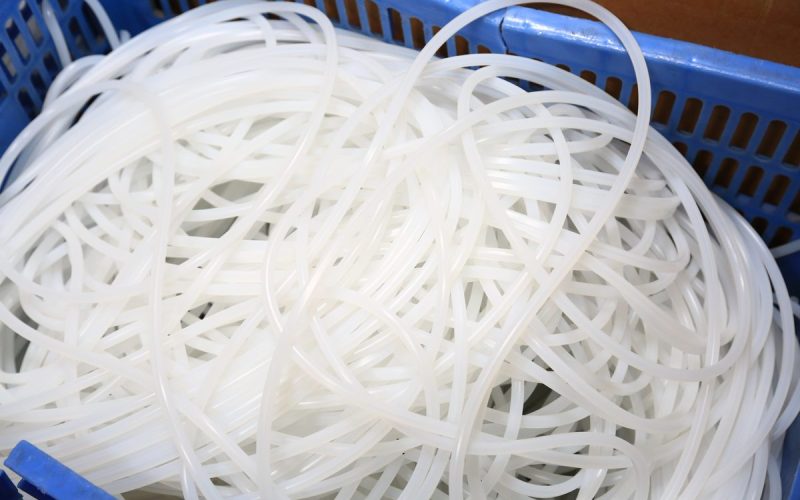
Extruded Silicone Tubing
Small-diameter tubing extruded to a consistent wall, then cut and packed to length.
View Case StudyReady to Start Your Precision Component Project?
Send us your drawing and requirements for an engineering review and quotation.