Case Study · CNC Machining
Machined Aluminium Housing
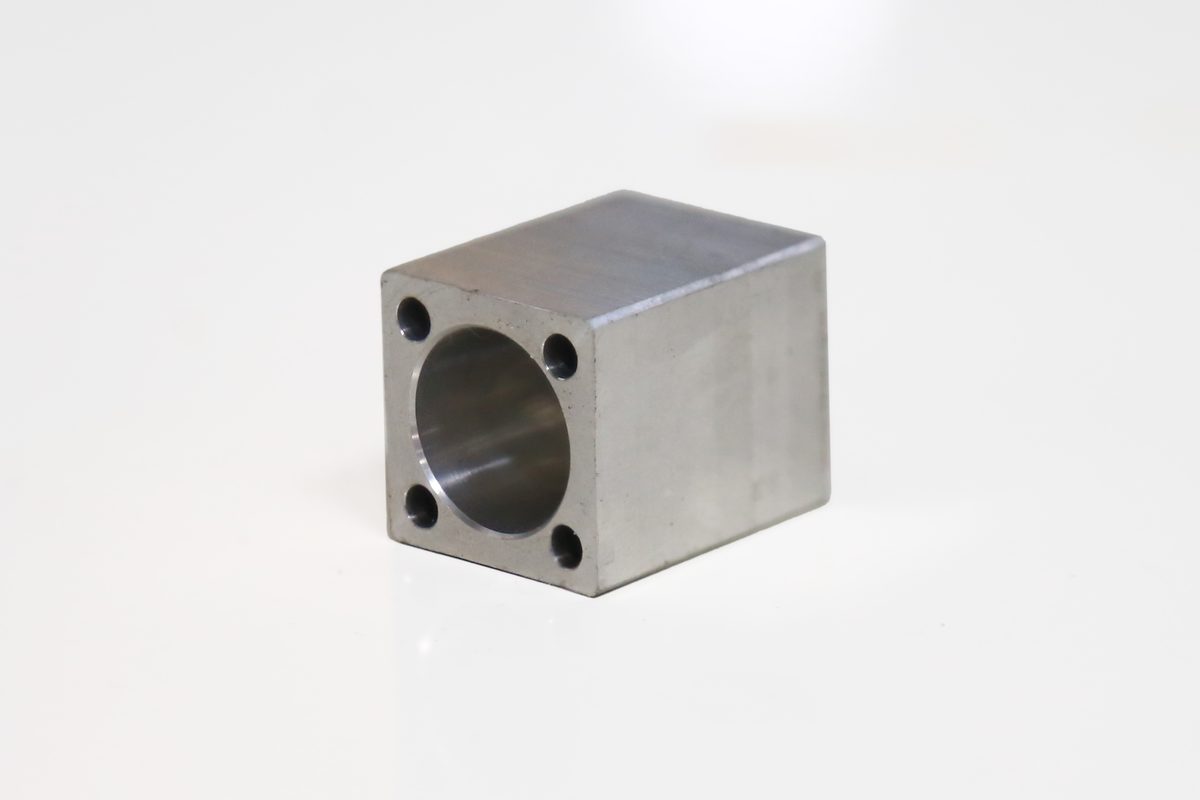
An automation housing with two bores that had to stay concentric to a sealing face — 0.02 mm over a 120 mm span, on a part that is machined on five sides.
Problem
Two setups, two datums, one leak
The customer had been buying the housing from a supplier who machined the bores in a second setup. Concentricity drifted between batches, and the seal leaked on roughly one part in twenty.
Rework was possible but expensive: the bore had to be opened up and sleeved, which changed the sealing face and required a new gasket each time.
Approach
One datum, one setup, one inspection
We re-quoted the part as a single-route job: the two bores machined in the same setup as the mounting face, on a 4-axis machine, then finished after anodizing so the coating thickness could not close the bore.
- Bores machined in one setup
- Anodizing before final bore sizing
- CMM report on first article
- Bore gauge check on every 10th part
Result
Leak rejects stopped, and the part got cheaper
The first batch passed leak testing without a single rework. The customer moved the annual volume to a single purchase order with a quarterly release schedule.
The change that mattered was not a new machine — it was removing the second setup that had been creating the variation.
Drawings and customer name stay confidential. Figures are given as a range where the exact value identifies the project.
More projects
Related case studies
Molded Plastic Enclosure
Two-part ABS enclosure with a gasket groove molded in, matched to a silicone seal.
View Case Study
Automation Fixture Bracket
Bracket machined from solid, flatness and hole position held for a locating fixture.
View Case Study
Extruded Silicone Tubing
Small-diameter tubing extruded to a consistent wall, then cut and packed to length.
View Case StudyReady to Start Your Precision Component Project?
Send us your drawing and requirements for an engineering review and quotation.